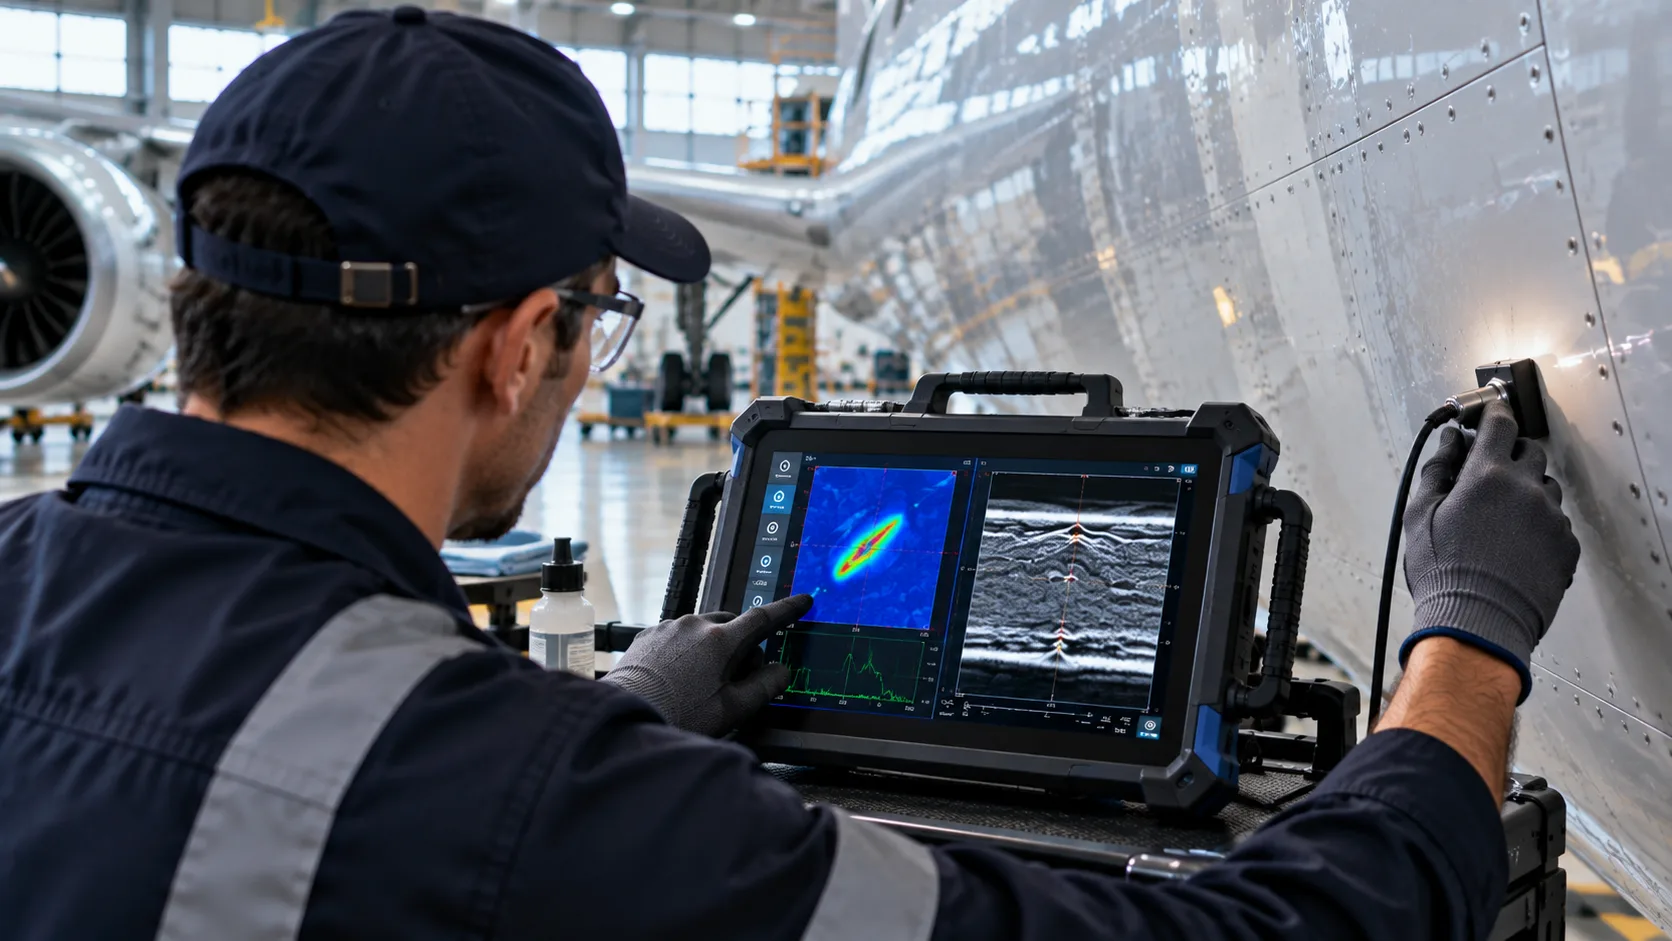
NDT inspection of fuselages is moving toward systems capable of combining different test methods on a single platform. A solution developed by Testia integrates Eddy Current Testing (ET) and Ultrasonic Testing (UT) to assess aluminum panels after blend-out operations, making it possible to verify both the presence of the protective cladding and the material’s residual thickness.
The approach addresses a structural integrity issue that is difficult to identify visually. In certain aeronautical structures, a layer of pure aluminum protects the high-strength alloy underneath. An overly deep mechanical repair can locally remove this protection and increase the base material’s exposure to corrosion.
NDT inspection of fuselages addresses damage that can go unnoticed
Aircraft surfaces can suffer scratches during manufacturing, operation, or maintenance. When this damage is corrected through blend-out, material is removed in a controlled manner until the discontinuity is smoothed. The challenge is to confirm that the procedure has not also removed an excessive amount of the cladding.
In the panels described by Aerospace Testing International, this cladding represents only about 2% to 4% of the sheet thickness, with approximate values of 0.04 to 0.40 mm. After machining, a localized loss may not be distinguishable to the naked eye.
This condition explains why non-destructive testing becomes important after the repair. Instead of relying solely on a surface assessment, the inspector can use the material’s physical properties to determine what remains beneath the surface.
Combining different techniques is a broader trend within NDT inspection in the aerospace industry, where ultrasound and eddy currents make it possible to address different mechanisms and discontinuities without altering the component.
Eddy Current detects changes in aluminum cladding
The first part of the assessment leverages differences in electrical conductivity between the aluminum cladding and the 2024 structural alloy. According to published technical data, at an operating frequency near 1 MHz, 2024 plates with cladding show conductivity values of approximately 26 to 36 MS/m, depending on thickness. When the cladding is no longer present, the reading drops to approximately 17 to 18 MS/m. This difference makes it possible to use Eddy Current to identify the boundaries of areas where the protective layer has been lost.
In practical terms, ET answers a first fundamental question: is the cladding still present after the blend-out? However, identifying the cladding does not, by itself, determine how much structural material remains. To answer that second question, ultrasound comes into play.
Ultrasound determines fuselage residual thickness
Ultrasonic Testing uses acoustic waves to assess the material and perform thickness measurements. In this case, its function is to quantify the residual thickness within the cavity created during the repair. The combination is complementary: Eddy Current identifies the cladding condition and UT measures the remaining material.
This integration reduces the need to use separate instruments for two related checks. The Smart UE1 EVO operates a 2 MHz ET probe and a 20 MHz UT probe from the same platform, while dedicated applications guide calibration, acquisition, and evaluation.
Testia also notes that the Smart UE1 family supports UT, ET, and resonance testing, along with applications for thickness measurement and cladding detection. The manufacturer states that the instrument is currently referenced in 185 Airbus NTM procedures.
What does integrating Eddy Current and ultrasound deliver?
Beyond reducing the number of devices, the integration aims to standardize how certain inspections are carried out.
The Clad Tool application incorporates calibration sequences and digital checks designed to reduce errors during evaluation. For more specialized inspections, another application makes it possible to map and export the geometric boundaries of areas where protection is missing. The solution described also considers different levels of intervention by NDT personnel.
Digitalization also supports traceability. Results stop being just a point reading and can become stored, comparable information—a shift that is also driving the development of digital NDT through automation, robotics, and data platforms.
Robotics and C-scans push inspection toward automation
The evolution does not end with portable instruments. For higher-volume manufacturing environments, the same methodologies are being adapted to automated systems. The configuration described includes a 1 MHz Eddy Current Array (ECA), a 10 MHz Ultrasonic Phased Array system, and six-axis robots moving on linear rails. The robot position can be synchronized with acquisition to automatically generate and analyze C-scans and associate geometric information with digital models.
This advance aligns with the evolution of phased-array ultrasound and open platforms in NDT, where coverage, repeatability, automation, and traceability are gaining greater weight in industrial inspection.
The integration of Eddy Current and ultrasound thus reflects a broader transition in NDT inspection of fuselages: moving from independent checks to digital workflows where different methods provide complementary information about the same area. In aeronautical applications, knowing whether the protective cladding remains and how much structural material is left after a repair makes it possible to turn a virtually invisible condition into measurable, traceable data.
Sources: Aerospace Testing International | Testia Smart UE1 | Airbus